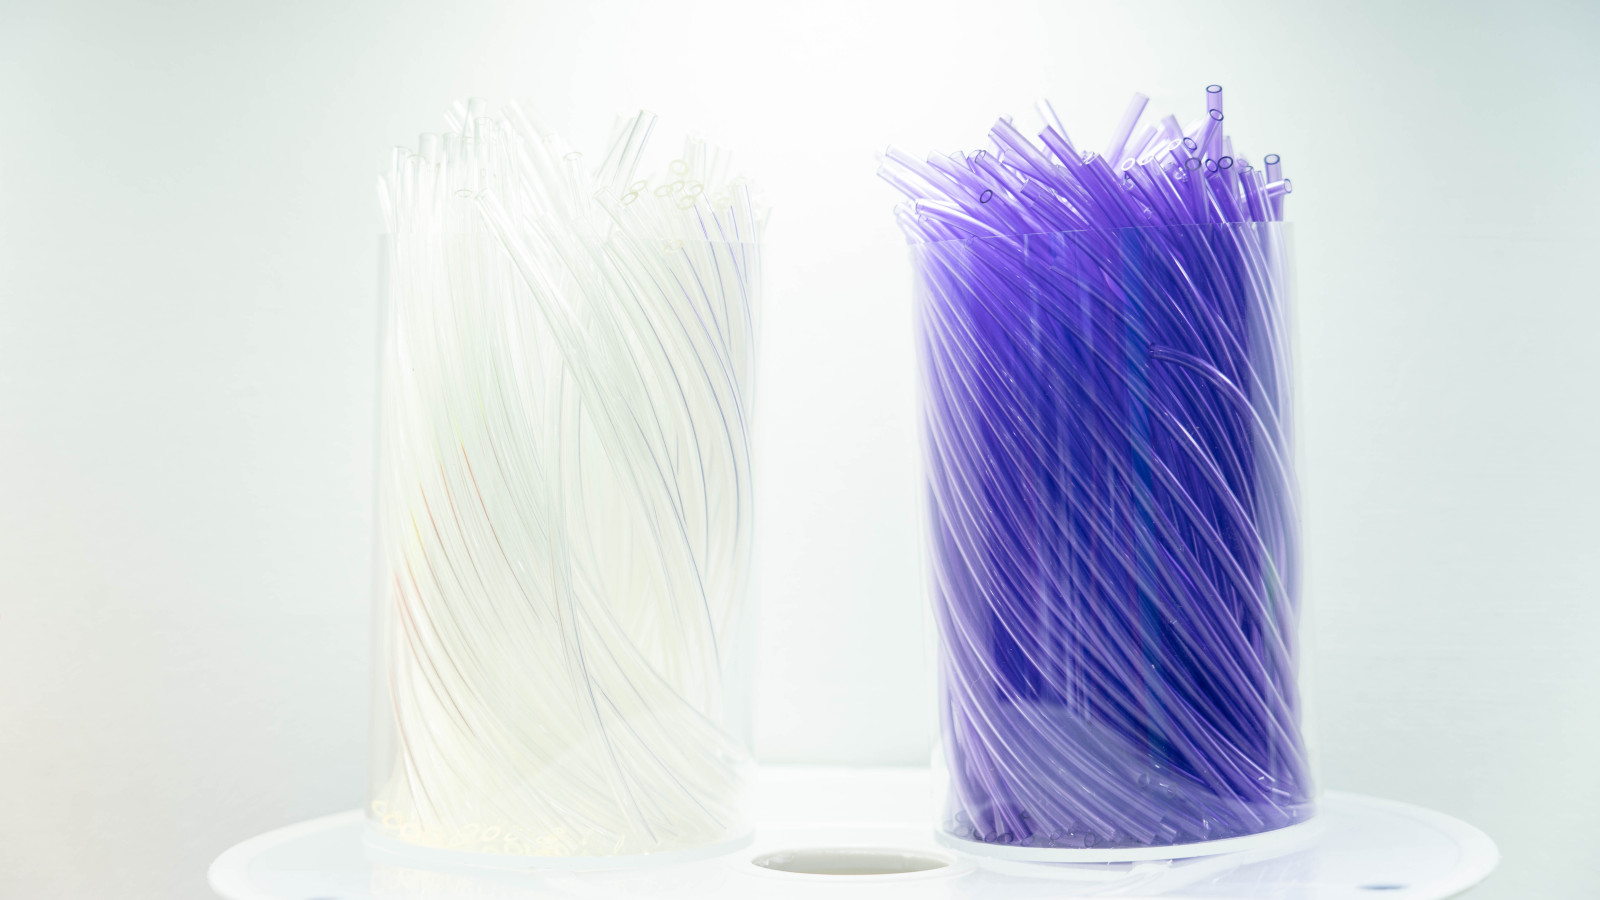
Thermoplastic polyurethane (TPU) tubing is a workhorse in industries ranging from medical devices to pneumatic systems, prized for its flexibility, abrasion resistance, and chemical durability. Yet even the best tubing fails—often prematurely and without obvious warning. In my years consulting on fluid handling and material selection, I’ve seen the same mistakes repeat across shops and labs. The cost isn’t just downtime; it’s safety risks, product contamination, and ballooning maintenance budgets. Below, I break down the five most common failure modes, backed by field data, and give you actionable steps to avoid each one.
TPU’s Achilles’ heel is its ester-based chemistry. While ether-based TPU offers better resistance, many standard grades (especially aromatic polyesters) are vulnerable to hydrolysis—a chemical breakdown when exposed to moisture and heat over time. A 2021 study in Polymer Degradation and Stability found that at 85°C and 85% relative humidity, ester-based TPU lost 70% of its tensile strength within 500 hours. I’ve seen medical device manufacturers ignore this, only to have tubing crack inside implantable pumps after six months of body-temperature exposure.
Preventive Steps:
Specify ether-based TPU for any application with sustained humidity >60% or water contact. It costs 10–15% more but extends service life by 3–5x.Kinking isn’t just a nuisance—it creates permanent stress points that lead to micro-cracks and eventual leakage. The most common cause? Designers and installers ignoring the minimum bend radius (MBR). For standard TPU, the MBR is typically 8–10 times the outer diameter (OD), but I’ve audited facilities where workers forced 6mm OD tubing into a 20mm radius curve—a 3.3x violation. Result: a 40% reduction in flow area and fatigue failure within 90 days of dynamic flexing.
Preventive Steps:
TPU resists many oils, greases, and diluted acids, but it’s no match for polar solvents like acetone, MEK, or concentrated sulfuric acid. In a 2020 industrial case study, a chemical plant used TPU tubing for a secondary containment line that occasionally saw isopropyl alcohol (IPA) washdowns. Within weeks, the tubing swelled by 15% in volume and turned sticky, causing blockages. The supplier’s data sheet listed “good” IPA resistance—at room temperature and short exposure. The reality: repeated 30-minute cleanings at 40°C accelerated chain scission.
Preventive Steps:
Cross-check every chemical in your process against the TPU grade’s compatibility chart, not the generic “good” column. Request a soak test with your exact fluid, at your max temperature, for at least 72 hours.Fatigue failure from repeated bending, twisting, or vibration is the #1 reason pneumatic tubing fails in automated machinery. A 2019 analysis of robotic arm breakages showed 62% occurred within 15mm of the fitting—the point where strain concentrates. Operators often overtighten compression fittings, creating local notches that act as crack initiation sites.
Preventive Steps:
Use torque wrenches for fittings. Over-tightening by just 1/8 turn can reduce fatigue life by half (verified in flex testing per ISO 7624).While less common indoors, TPU exposed to direct sunlight embrittles within 18 months—a fact many solar tracker and agricultural irrigation users learn too late. Ultraviolet light breaks the polymer’s chain bonds, turning a shiny, flexible tube into a chalky, cracked straw. My own field notes from a 2022 Texas solar farm showed a 90% loss in elongation at break after just 11 months of unshielded UV exposure.
Preventive Steps:
Specify UV-stabilized TPU (often marked “outdoor grade”) for any outdoor or window-proximity installation. These include additives that absorb UV—typically raising cost by 5–8%.Bringing this back to practical reality: I frequently see buyers gravitate to the cheapest TPU quote, ignoring the total lifecycle cost. Let’s math it out. A failed 10-foot section in a food processing line costs roughly $4,000 in lost product, labor, and re-certification. A premium ether-based, UV-stabilized TPU might cost $120 more upfront—that’s a 33x return on prevention. Over 90% of tubing failures are avoidable with proper spec, installation, and maintenance. Ask for a material certificate and compatibility test data before you buy. Your equipment, your uptime, and your bottom line will thank you.
One pivot worth considering: when you need a partner who understands these nuances, look for a supplier that publishes detailed chemical resistance charts and offers custom cut-to-length options with same-day shipping—not just a bulk spool. The right manufacturer will also walk you through bend radius calculations for your specific fitting torque, not just throw a generic datasheet back at you. That’s the difference between a vendor and a reliability collaborator. Choose accordingly.